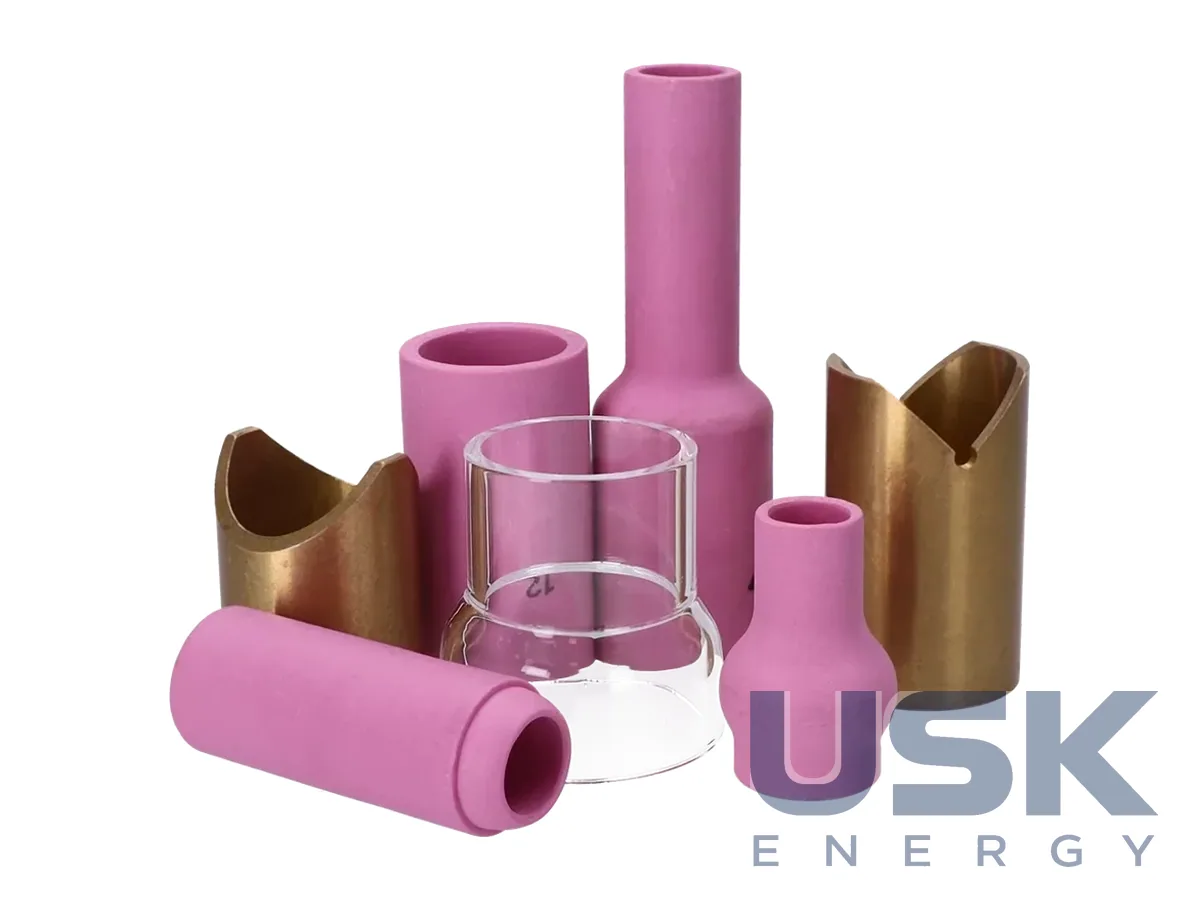
consumable parts for MIG/MAG and TIG torches
Country: Austria · Model: MIG/MAG, TIG consumables
Original consumable parts for MIG/MAG and TIG torches include three types of contact tips, about 300 gas nozzles, six types of wire liners and TIG accessories. Process stability and production costs depend on them, because the parts work in heat, spatter and under constant abrasion by the wire. The tips, nozzles, liners and special shapes are developed in Austria.
- MIG/MAG
- contact tips E-Cu, CuCrZr, WQ; about 300 gas nozzles; 6 types of liners (steel, CrNi, Teflon, graphite, bronze)
- TIG
- gas nozzles (including “champagne” and narrow ones), gas lenses, meshes, TFC system, A and P systems
- Application materials
- steel, CrNi, aluminium, CuSi
- Development
- Austria
Technical specifications
| MIG/MAG | contact tips E-Cu, CuCrZr, WQ; about 300 gas nozzles; 6 types of liners (steel, CrNi, Teflon, graphite, bronze) |
|---|---|
| TIG | gas nozzles (including “champagne” and narrow ones), gas lenses, meshes, TFC system, A and P systems |
| Application materials | steel, CrNi, aluminium, CuSi |
| Development | Austria |
| Customs codes (for reference) | |
| HS code | 8515.90 |
| UKTZED code (Ukraine) | 8515900000 |
| CN code (EU) | 85159000 |
Specifications are taken from the manufacturer’s technical documentation. Updated . Customs codes are for reference only; the final code is determined at customs declaration for the specific model.
Description
The E-Cu tip, made of pure electrolytic copper, has high electrical and thermal conductivity but softens at about 260 °C, so it is used for low currents in manual welding. CuCrZr, made of a copper–chromium–zirconium alloy, withstands up to 500 °C and works at medium and high currents in manual and robotic torches for steel, CrNi, aluminium and CuSi. The WQ has a tungsten-copper core in a CuCrZr body for severe conditions, and the Contec for aluminium and CuSi gives 100 % constant contact and an unchanging TCP point. Insulated nozzles for steel and CrNi are cleaned with a reamer or a magnetic pulse, and coated nozzles for aluminium and CuSi with a brush. Liners come in uncoated and coated steel, CrNi, Teflon, graphite and bronze, and for aluminium there are also gas distributors.
How to choose
The tip type is chosen by current and welding method: E-Cu for manual work at low currents, CuCrZr for medium and high currents, WQ for severe duty. The liner is selected to suit the wire material from six types or a combination of them. In TIG, the A system with a push-on nozzle is convenient where nozzles are changed often, and the P system with a screw-on nozzle gives maximum stability.
Request a price and lead time
consumable parts for MIG/MAG and TIG torches. We reply within one business day.
Or email office@usk.ua or call +38 (044) 339-50-20.
FAQ
Which contact tip should be chosen for robotic welding of aluminium?
For aluminium and CuSi the manufacturer offers the special Contec tip. For medium and high currents in robotic torches, CuCrZr, which withstands up to 500 °C, is also suitable.
Which TIG gas nozzle shape should be chosen?
The “champagne” nozzle gives even gas distribution, and the “champagne glass” gives a better view of the welding point. There are also narrow and standard nozzles and nozzles for spot welding.
What are the gas lens and gas mesh for in a TIG torch?
The gas lens forms a laminar flow of shielding gas, and the mesh protects the lens itself. Torch caps come in different lengths, and tungsten electrodes with different alloying additions.
How many MIG/MAG gas nozzles are in the range?
About 300, including narrow ones for better access, reinforced Heavy Duty ones and coated nozzles for aluminium.
Similar products
 iQ 1500 / iQ 3000 / iQ 4500iQ 1500 / iQ 3000 / iQ 4500 high-precision plasma systems 20–450 A for CNC cutting
 Smart Focus 130 / 200 / 300 / 400Smart Focus 130 / 200 / 300 / 400 plasma systems 35–400 A for machine cutting
 SmartSYNCPlasma torches with RFID for Powermax SYNC
 Duramax / Duramax Lock / Duramax HyampPlasma torches for Powermax
REQUEST
Need a price, lead time or replacement?
Send us a request and we will confirm the configuration, lead time and delivery terms. We reply by email.