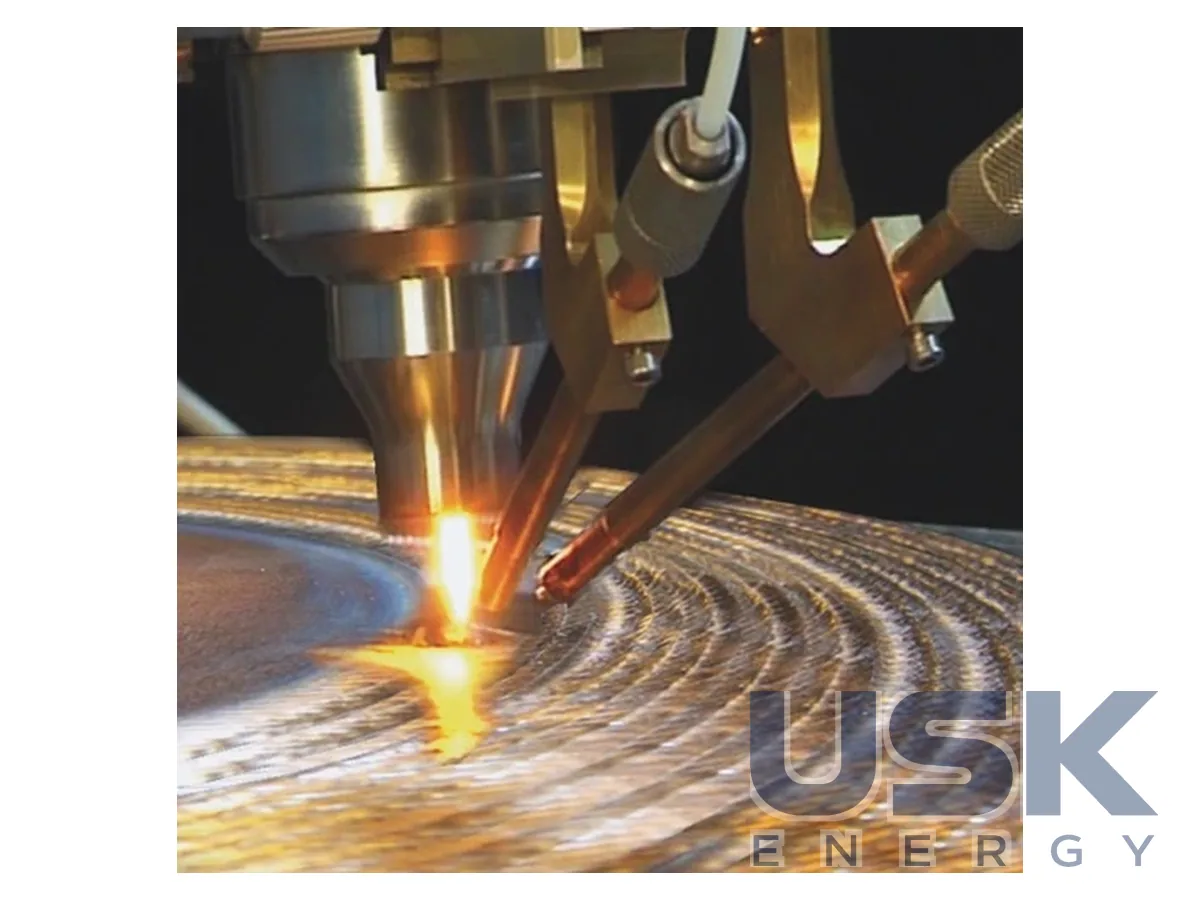
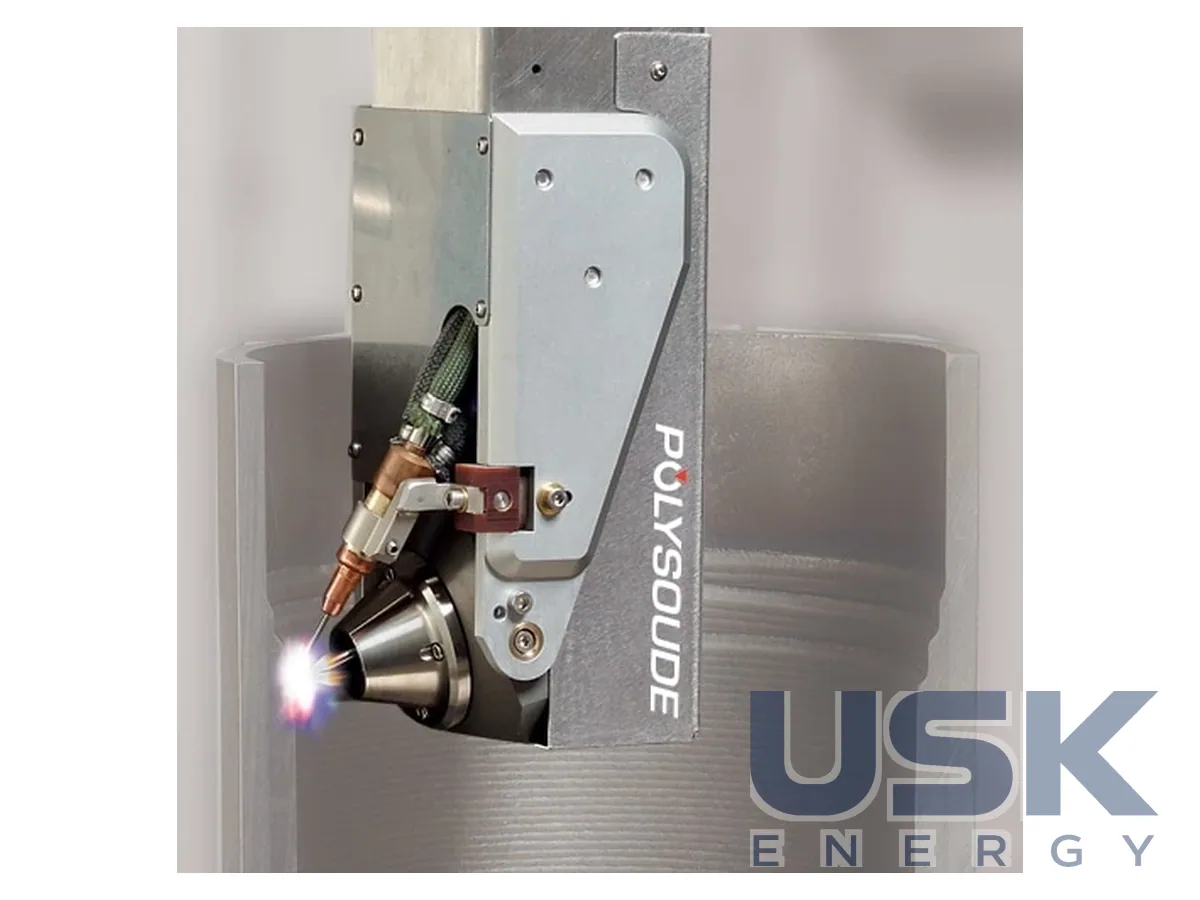
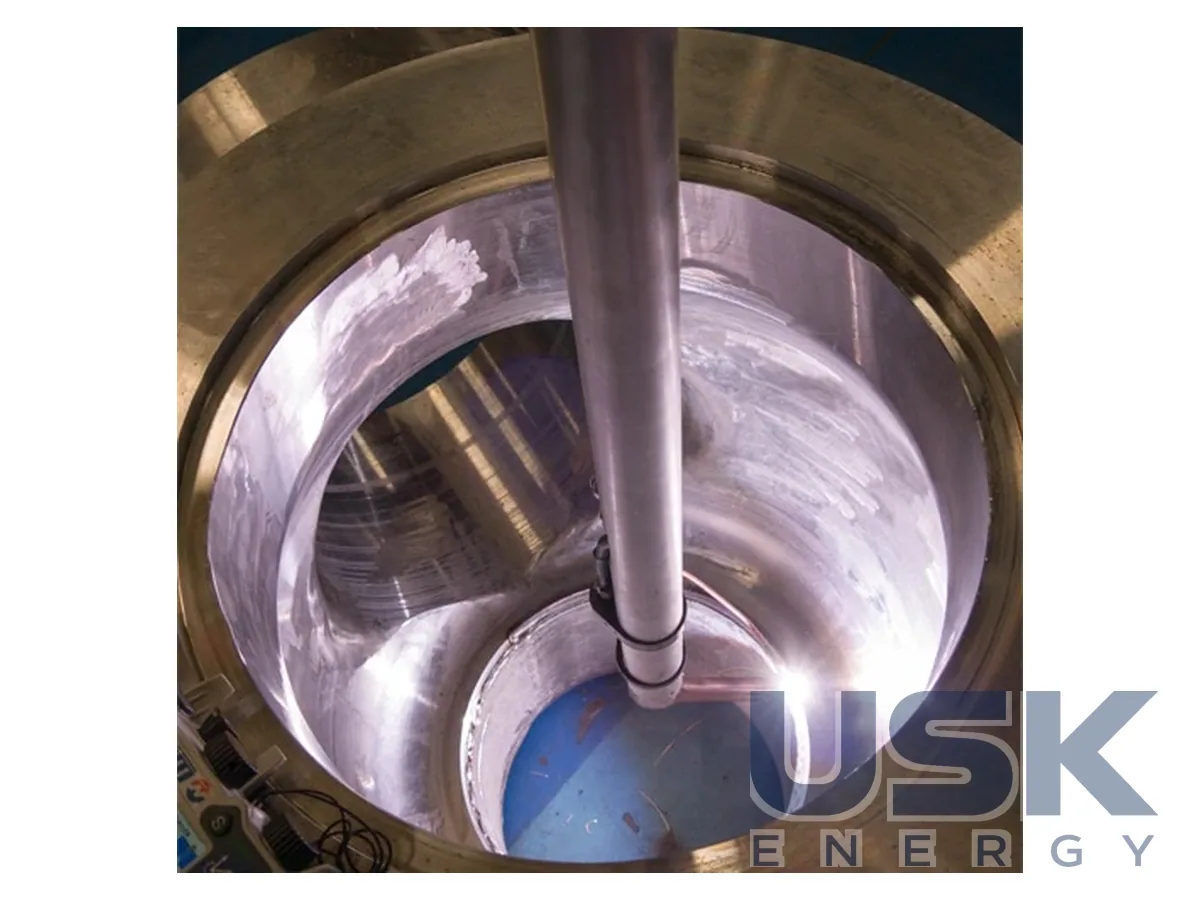
TIGer / TIG HW cladding torches and lances (single, TWIN, MSO)
Country: · Model: TIGer, TIG HW
TIGer and TIG HW are torches and lances for automatic cladding with a non-consumable electrode and hot wire. The layer is 1.5–3.5 mm thick, and the TIGer deposition rate is 2.5–6 kg/h. They are installed on PolyClad cladding machines, column-and-boom units and SPX heads.
- Process
- TIGer (two electrodes, hot wire) or TIG HW
- Layer thickness
- 1.5–3.5 mm (TIGer)
- Deposition rate
- 2.5–6 kg/h, speed 70–90 cm/min (TIGer)
- Dilution
- ≈12 % in the first layer, 1.5–2 % from the second
Technical specifications
| Process | TIGer (two electrodes, hot wire) or TIG HW |
|---|---|
| Layer thickness | 1.5–3.5 mm (TIGer) |
| Deposition rate | 2.5–6 kg/h, speed 70–90 cm/min (TIGer) |
| Dilution | ≈12 % in the first layer, 1.5–2 % from the second |
| Versions | single torch, lance, TWIN lance, MSO with motorized electrode stick-out |
Specifications are taken from the manufacturer’s technical documentation. Updated .
Description
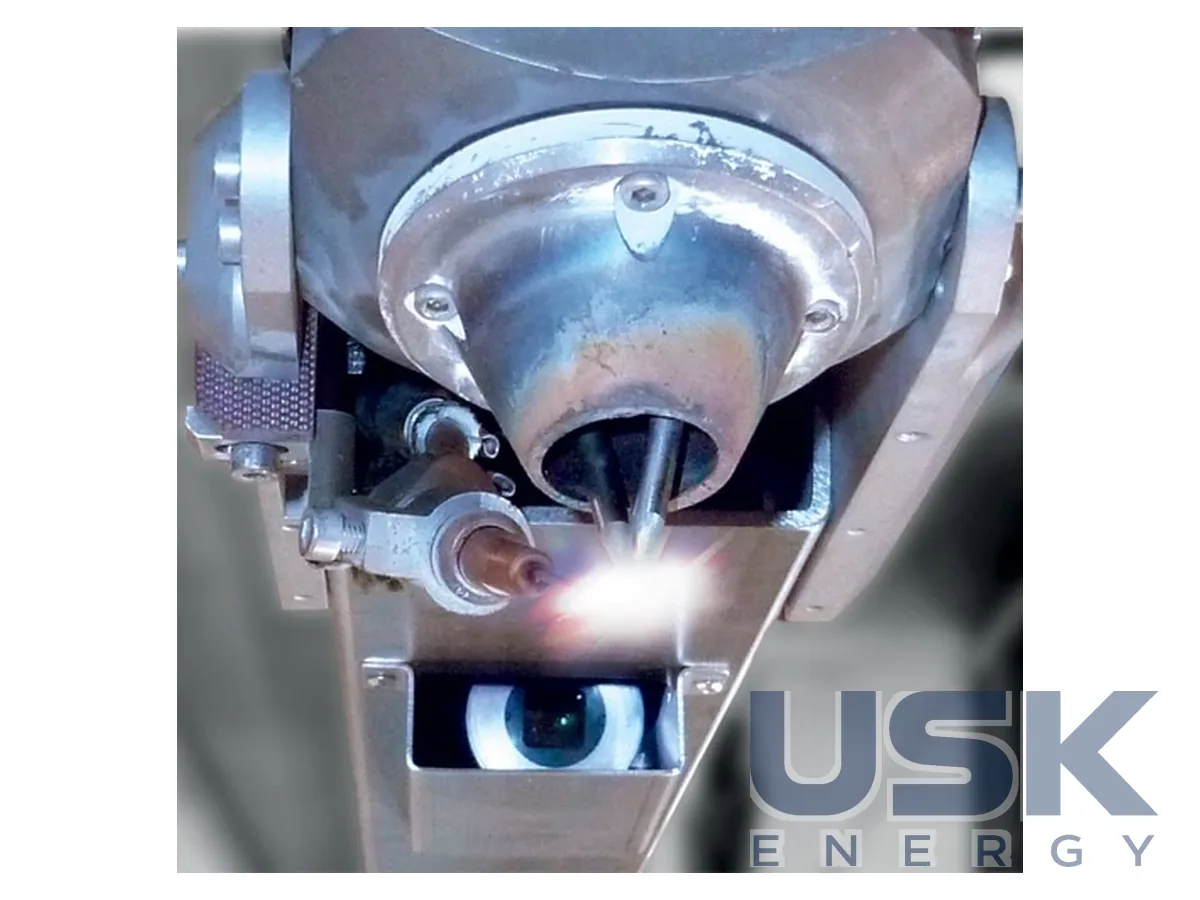
In the TIGer process two arcs from two tungsten electrodes sit side by side and merge into one with a combined power, while the wire is heated by Joule heat from a third current source. The process was presented in 2013 as a development of TIG Hot Wire. The low arc pressure makes it possible to clad at high speed even at high currents, and pure argon is usually enough, without special tungsten grades. The cladding speed is 70–90 cm/min in the brochure, and on the website 500–1000 mm/min and more than 1700 mm/min, up to 2000 mm/min with 1.2 mm wire in some applications. In the flat position PA it is 5.8 kg/h at 85 cm/min, in the horizontal position PC 4.4 kg/h, which is about three times higher than TIG HW. Dilution is about 12 % in the first layer and 1.5–2 % from the second, and the cost per kilogram of metal is 20–50 % lower.
How to choose
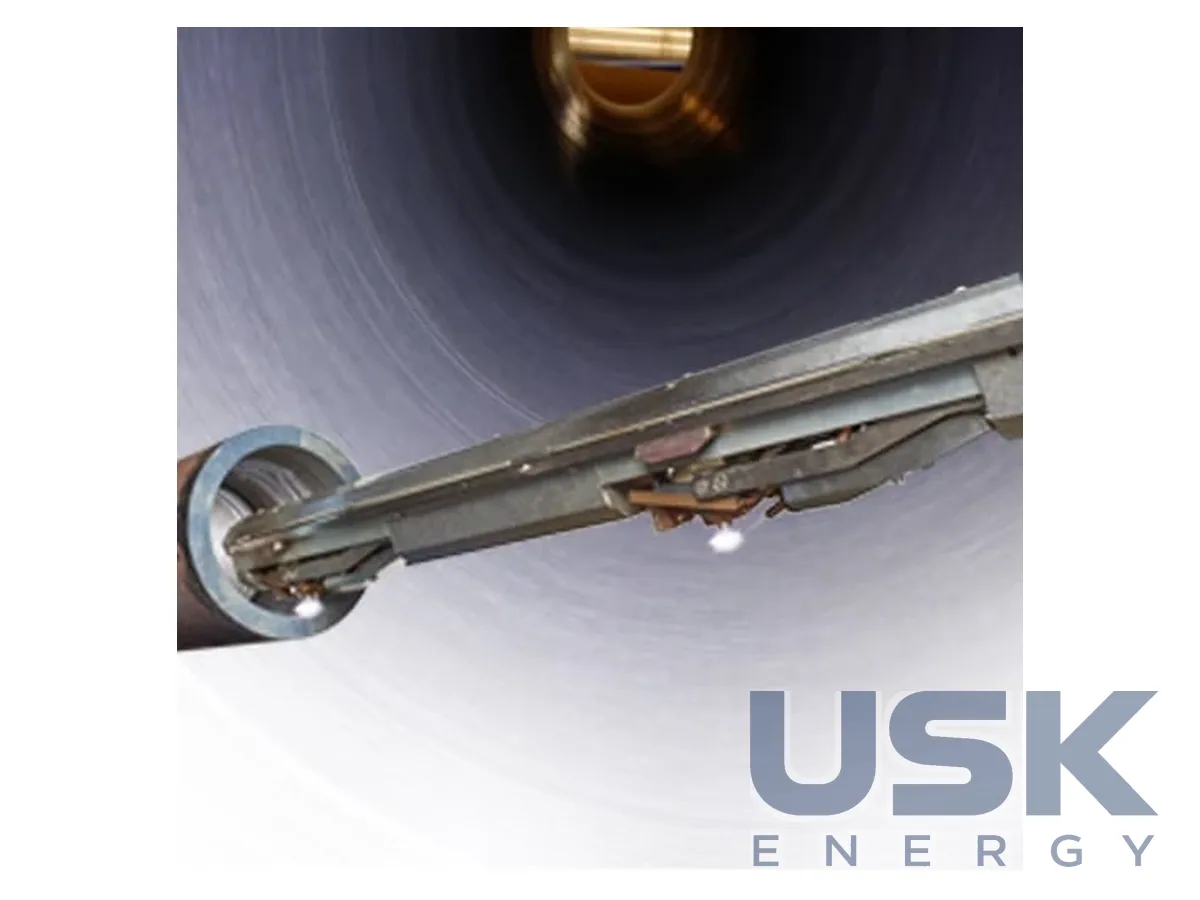
The torch type depends on the bore. TIGer single torch is for short and medium lengths, TIGer Lance for medium and large bores, and TIGer TWIN torch for clad tubes up to 18 m long. The classic TIG HW single torch and TIG HW lance are taken for small bores, and the TIG HW TWIN torch for tubes over the full length. MSO TIG HW has a motorized programmable electrode stick-out for continuous cladding of ring grooves. TIGer lances suit tubes with an inside diameter from 100 mm.
Request a price and lead time
TIGer / TIG HW cladding torches and lances (single, TWIN, MSO). We reply within one business day.
Or email office@usk.ua or call +38 (044) 339-50-20.
FAQ
How does TIGer differ from ordinary TIG HW?
Two electrodes are used and the arcs merge into one, so productivity is about three times higher than TIG HW.
What are the layer thickness and productivity of TIGer?
The layer is 1.5–3.5 mm and productivity is 2.5–6 kg/h according to the manufacturer.
What shielding gas is needed for TIGer?
Pure argon is usually enough, and special tungsten grades and exotic mixtures are not needed.
What tubes are TIGer lances suitable for?
For tubes with an inside diameter from 100 mm, and the TWIN lance welds clad tubes up to 18 m long.
What dilution does TIGer give?
About 12 % in the first layer and 1.5–2 % starting from the second.
Similar products
 Fortis 270 / 320 / 400 / 500MIG/MAG welding power source 270–500 A (multiprocess)
 TPS/i (270i C, 320i C, 320i, 400i, 500i, 600i)MIG/MAG welding system 270–600 A
 iQ 1500 / iQ 3000 / iQ 4500iQ 1500 / iQ 3000 / iQ 4500 high-precision plasma systems 20–450 A for CNC cutting
 Smart Focus 130 / 200 / 300 / 400Smart Focus 130 / 200 / 300 / 400 plasma systems 35–400 A for machine cutting
REQUEST
Need a price, lead time or replacement?
Send us a request and we will confirm the configuration, lead time and delivery terms. We reply by email.