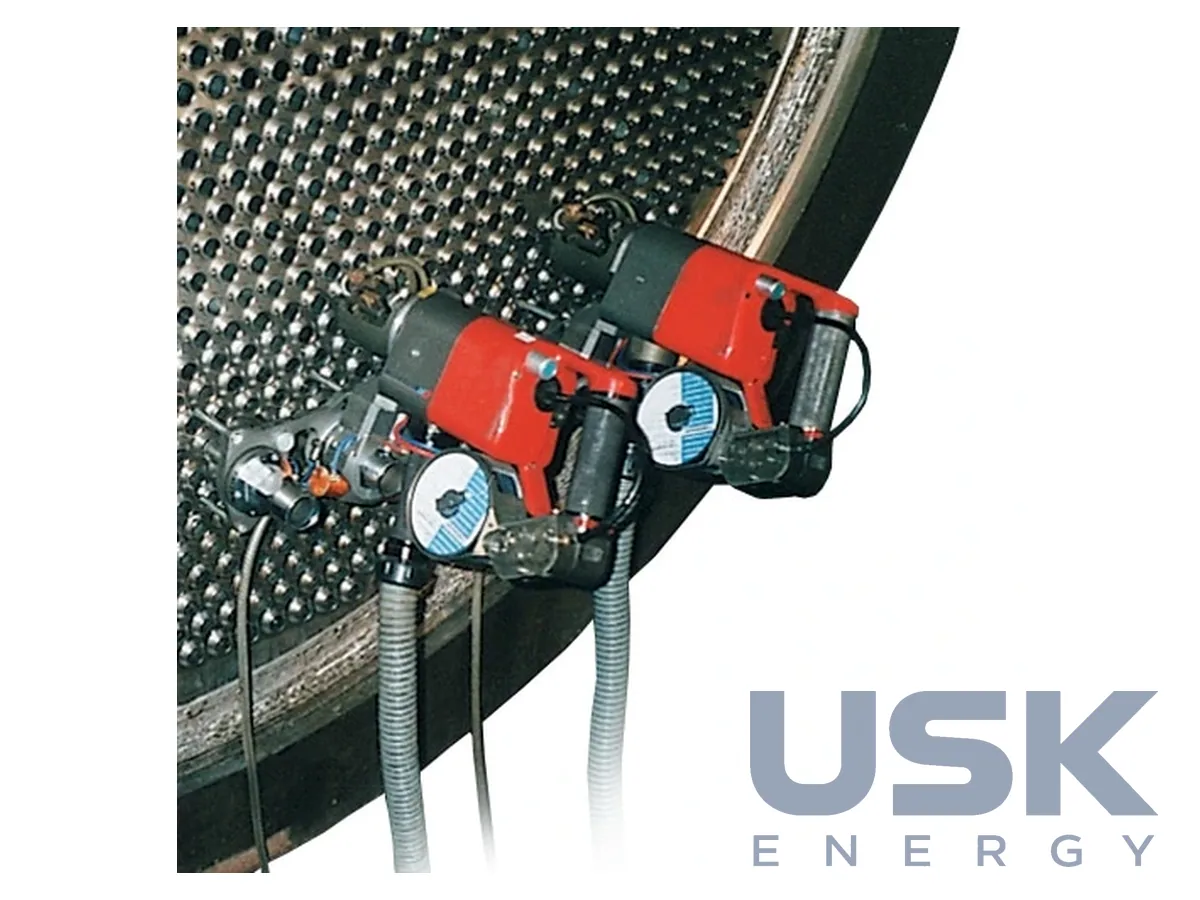
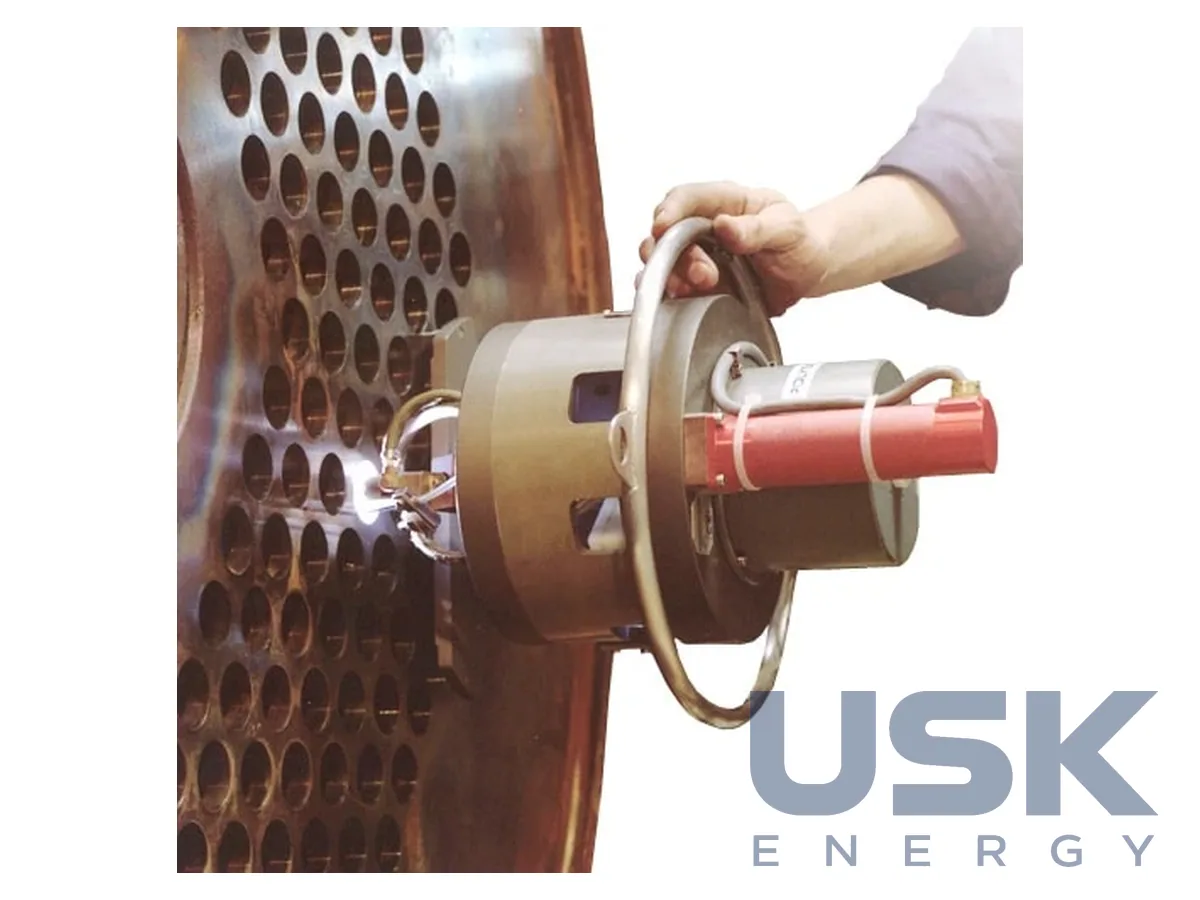
TP 60 / SPX Compact heads for multipass tube-to-tubesheet welding
Country: · Model: TP 60 / SPX Compact
TP 60 and SPX Compact are two heads for multipass orbital welding of tube-to-tubesheet joints by TIG with filler wire. TP 60 is intended for critical joints and has an adaptive sensor, while SPX Compact rotates the torch endlessly and shifts it along the X/Y axes under a program. Both complement the standard TS 34 and TS 8/75 heads in heat exchangers and reactors.
- TP 60
- with adaptive sensor, for critical applications (urea reactors made of super duplex steel)
- SPX Compact
- endless rotation, programmable X/Y torch positioning, multipass welding without stopping
- Process
- TIG with wire
Technical specifications
| TP 60 | with adaptive sensor, for critical applications (urea reactors made of super duplex steel) |
|---|---|
| SPX Compact | endless rotation, programmable X/Y torch positioning, multipass welding without stopping |
| Process | TIG with wire |
Specifications are taken from the manufacturer’s technical documentation. Updated .
Description
TP 60 is designed for critical applications, for example building urea synthesis reactors from super duplex steels, where tube-to-tubesheet welds face especially strict quality and repeatability requirements. According to the manufacturer, the head is fitted with an adaptive sensor and additional process monitoring functions. In SPX Compact the torch rotates continuously because current, gas and coolant are fed through a rotating manifold. The cable does not have to be unwound back, so multipass welding runs without a pause for the return. Programmable torch shifting between passes makes it possible to lay them in a set order. Both heads are controlled by P6 and PC series power sources, and the wire is fed by Polyfil mechanisms.
How to choose
The choice starts with the weld requirements. For ordinary joints in a heat exchanger TS 34 or TS 8/75 is enough, while TP 60 and SPX Compact are taken where process monitoring and multipass cladding with a full torch revolution are needed. Most tubes in heat exchangers have an outside diameter of 19.05 to 50.8 mm with a wall thickness of 1.65 to 4.5 mm. The diameter ranges, current and weight for these two heads are not given in the sources, so they are clarified for the specific tubesheet.
Request a price and lead time
TP 60 / SPX Compact heads for multipass tube-to-tubesheet welding. We reply within one business day.
Or email office@usk.ua or call +38 (044) 339-50-20.
FAQ
How does TP 60 differ from SPX Compact?
TP 60 is aimed at full process control and has an adaptive sensor. SPX Compact is distinguished by endless torch rotation and programmable X/Y positioning.
Which welding process do these heads use?
Both work by TIG with filler wire. They are controlled by P6 and PC series power sources, and the wire is fed by a Polyfil mechanism.
Why is endless torch rotation needed in SPX Compact?
Because of the rotating manifold the cable does not twist, so stops for unwinding are not needed. A multipass weld is made in one continuous cycle.
Which tubes are usually welded in heat exchanger tubesheets?
Mostly those with an outside diameter of 19.05 to 50.8 mm and a wall thickness of 1.65 to 4.5 mm.
Which reactors is the TP 60 head intended for?
For critical units, for example urea synthesis reactors made of super duplex steels.
Similar products
 Fortis 270 / 320 / 400 / 500MIG/MAG welding power source 270–500 A (multiprocess)
 TPS/i (270i C, 320i C, 320i, 400i, 500i, 600i)MIG/MAG welding system 270–600 A
 iQ 1500 / iQ 3000 / iQ 4500iQ 1500 / iQ 3000 / iQ 4500 high-precision plasma systems 20–450 A for CNC cutting
 Smart Focus 130 / 200 / 300 / 400Smart Focus 130 / 200 / 300 / 400 plasma systems 35–400 A for machine cutting
REQUEST
Need a price, lead time or replacement?
Send us a request and we will confirm the configuration, lead time and delivery terms. We reply by email.